
Performance cap color tolerance is the agreed limit for how far a material, component, logo, or production lot may differ from an approved color standard. Buyers need this control because one cap can combine woven shell fabric, mesh, sweatband, visor cover, thread, heat transfer, patch, and plastic trim. Each material reflects light differently, even when suppliers use the same color name.
A workable specification links an approved physical standard to a named visual setup, instrument formula, measurement conditions, component map, sampling plan, and decision owner. Add those points to the brief for a custom performance cap before lab dips, strike-offs, and logo trials begin.
Separate color tolerance from colorfastness
Color tolerance asks whether two specimens match closely enough at the time of inspection. Colorfastness asks how a color changes after exposure to light, washing, perspiration, rubbing, water, or another stated condition. A fabric can match the approved shade at delivery and still perform poorly in a colorfastness test. It can also pass a fastness requirement while its starting shade misses the brand standard.
Keep the two decisions in separate report fields. The existing performance cap colorfastness guide explains exposure tests and approval records. This guide covers the starting color match and the variation allowed across samples and bulk production.
| Buyer question | Control needed | Evidence retained |
|---|---|---|
| Does the fabric match the intended brand color | Approved standard and defined viewing conditions | Dated physical standard plus visual and instrument record |
| Do front, side, and visor materials look coherent | Component-to-component comparison on the assembled cap | Signed sample and component map |
| Does the logo match its artwork reference | Process-specific thread, ink, film, silicone, or patch standard | Approved strike-off or decorated panel |
| Does bulk stay within the released range | Lot sampling and shade grouping rule | Roll or lot readings and release decision |
| Will the color resist use and care | Separate colorfastness test plan | Method-specific laboratory report |
Build an approval standard that survives handoffs
A screen image or color name is a poor production standard. Monitors, office printers, camera settings, file profiles, and room lighting can shift the appearance. Start with the brand's specified color reference, then create a controlled physical standard for each material and process route.
Identify the standard with a style, component, color code, material article, supplier, finish, approval date, and revision. Protect it from direct light, dirt, moisture, folding, and repeated handling. Replace a worn or faded reference through a documented approval rather than quietly swapping it.
When a brand uses a digital color target, record the color space, profile, viewing assumptions, and the route used to translate that target into textile, thread, ink, or molded trim. The physical approval remains the practical comparison point for bulk production.

Use visual review and instrument data together
Visual review finds issues that a single number may miss, such as patchiness, streaks, mottling, panel-to-panel imbalance, gloss differences, or an objectionable hue direction. Instrument readings make repeated comparisons easier and create a traceable record. Use both where the brand, material, and order risk justify them.
ISO 105-J03 from 2009 describes a textile method for calculating color differences between specimens of the same material measured under the same conditions. The official ISO record says the standard was reviewed and confirmed in 2025. Its scope also allows a maximum tolerance to be set according to the closeness of match needed for the end use.
ال 2022 CIEDE2000 standard defines a formula intended to improve how calculated differences relate to perceived differences in lightness, chroma, and hue. A report should name the formula used. Results from CMC, CIEDE2000, and simple CIELAB distance are different data and should not be mixed under one unlabeled delta value.
| Review route | Useful purpose | Required controls |
|---|---|---|
| Visual assessment | Judge whole-product acceptability, direction, texture effects, and panel balance | Named light source, neutral surround, viewing geometry, trained assessor, and approved standard |
| Spectrophotometer reading | Compare specimens and retain numerical lot records | Instrument mode, aperture, illuminant, observer, measurement count, backing, and formula |
| Assembled-cap review | Check different materials and decorated areas in product form | Released sample, fixed orientation, viewing distance, and component map |
| Brand merchandising review | Confirm the intended commercial appearance across a range | Season palette, neighboring products, final materials, and named approver |
Instrument values only become comparable when specimens are measured under consistent conditions. Record whether the material is folded or single-layer, the backing color, face direction, aperture, number and location of readings, instrument geometry, inclusion or exclusion of specular reflection, illuminant, observer, and color-difference formula.
Condition specimens under the agreed laboratory atmosphere when the method or brand procedure requires it. Lay textured, brushed, ribbed, or directional fabric in the same orientation. A rotated specimen can produce a different visual result because the surface directs light differently.
Visual assessment also needs a repeatable setup. Name the primary light source and any secondary metamerism check. Use a neutral viewing surround and keep strongly colored clothing or nearby samples away from the viewing field. Compare the standard and specimen side by side, changing positions when the procedure calls for it.
Map every visible component before sampling
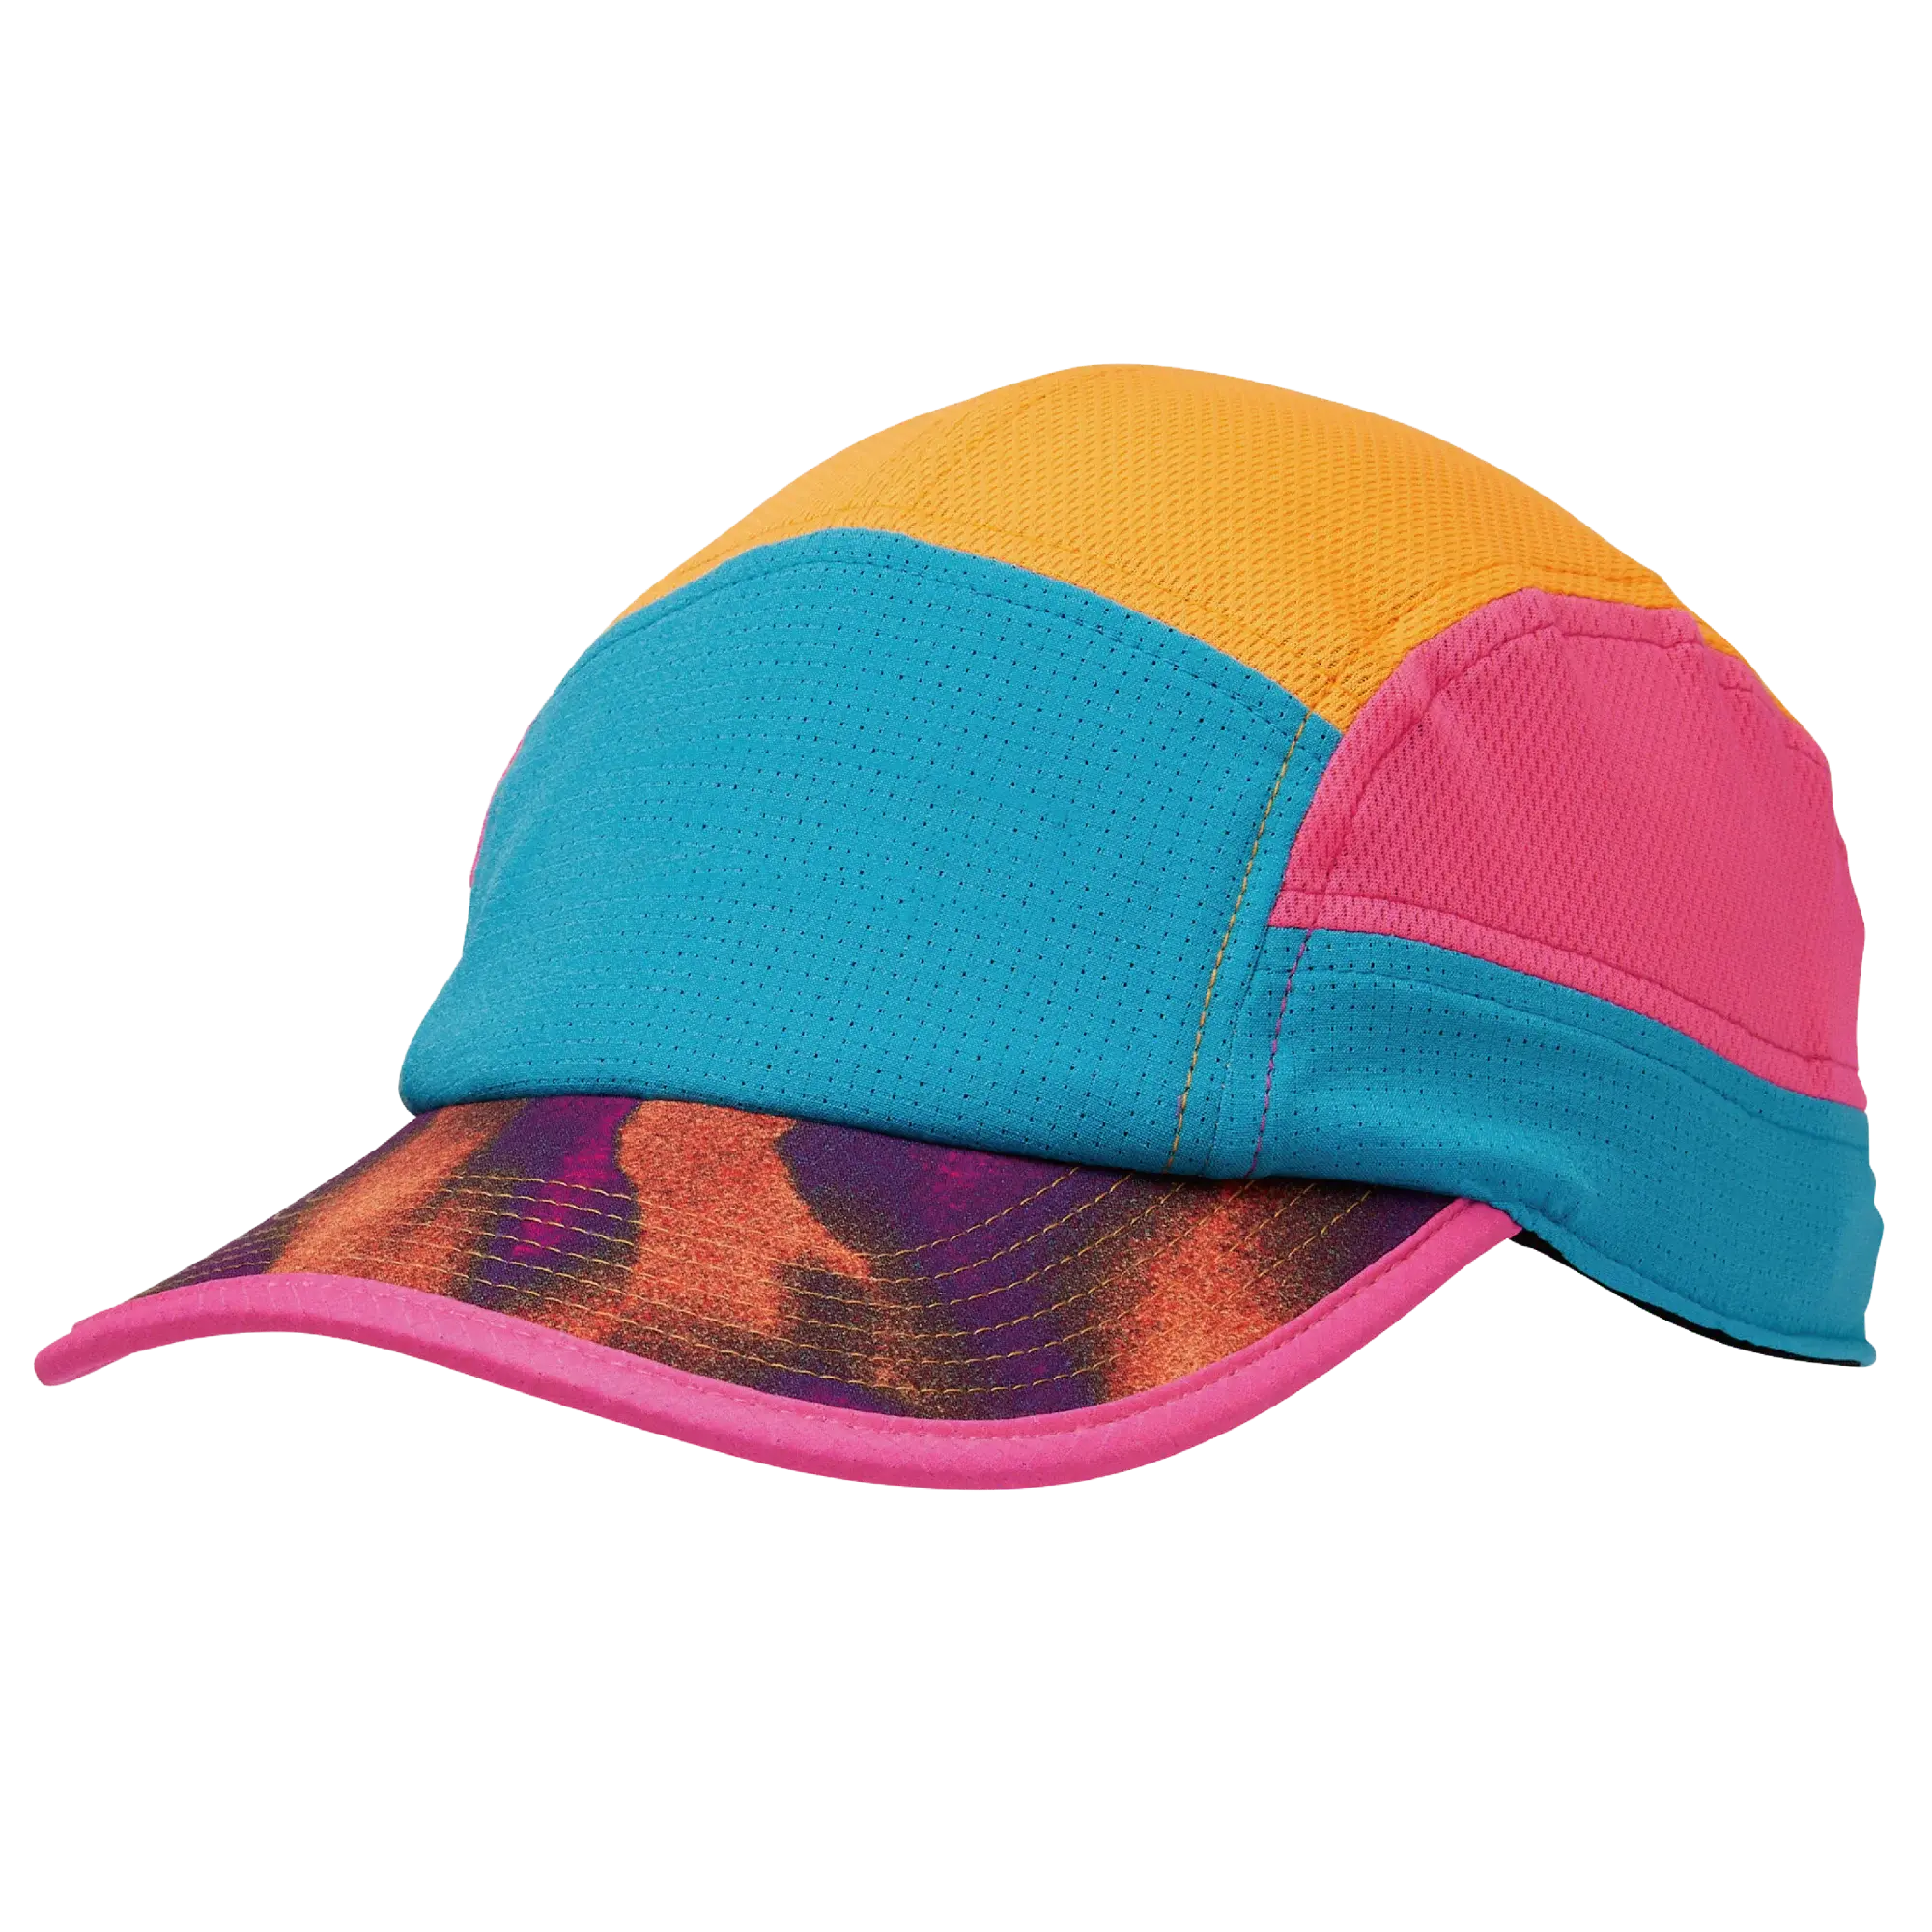
A performance cap rarely uses one material. Mark the shell panels, visor top and underside, button, eyelets, mesh, sweatband, seam tape, piping, closure, thread, label, logo, and patch edge on the artwork or bill of materials. State which components must match, which may use an intentional contrast, and which have their own standard.
Do not expect identical numerical readings from unrelated surfaces without first confirming that the comparison is meaningful. A matte woven shell, glossy silicone logo, embroidery thread, and molded plastic buckle interact with light in different ways. Approve each process against its intended reference, then judge their appearance together on the cap.
Write tolerances around a real end use
No single color-difference limit suits every shade, material, finish, logo process, and brand position. A small numerical difference may look objectionable in a neutral gray or across adjacent panels, while a larger reading may be acceptable on a textured or multicolored surface. Fluorescent, very dark, very light, metallic, heathered, and printed materials may need their own route.
Build the acceptance range from approved development samples, brand judgment, supplier capability, measurement repeatability, end use, and the cost of a mismatch. State whether the limit applies to each reading, the specimen average, the difference between rolls, the difference within one roll, or a combination.
| Specification field | Decision to record | Common source of dispute |
|---|---|---|
| Reference | Physical master, approved lab dip, or approved production standard | Comparing bulk with an unapproved screen image |
| Formula | Named calculation and parameter settings | Reporting only a delta symbol and number |
| Setup | Instrument, aperture, backing, illuminant, observer, and specimen orientation | Changing the setup between approval and bulk |
| Limit | Maximum, average rule, individual rule, and shade direction restrictions | Using an unwritten factory convention |
| Scope | Material, component, color route, supplier, and finish covered | Extending one approval to a different construction |
| Disposition | Approver, hold point, resubmission route, and failed-lot action | Cutting material before the result is released |
Place these fields in the performance cap tech pack and use the same color and material codes in the bill of materials, sample comments, purchase order, laboratory request, and inspection record.
Approve lab dips, strike-offs, and complete samples
Use lab dips for dyed textile routes, strike-offs for print or transfer routes, thread cards or stitched panels for embroidery, and molded or cast samples for plastic and silicone parts. Review submissions on the intended base material because ink, adhesive, film thickness, heat, pressure, and substrate color can shift the result.
Once individual components are acceptable, build a production-representative sample. Check it under the agreed primary light and any secondary light used by the brand. Review the cap from the front, sides, back, top, and underside. Pay close attention to adjoining panels and large logo areas.
Sign and date the final physical reference, record instrument data, and attach the approval to the sample revision. The sample approval checklist helps connect materials, decoration, fit, construction, and comments before the order moves forward.
Control shade groups before and during cutting
Bulk fabric can vary between dye lots, rolls, and positions within a roll. Inspect incoming material before cutting and keep roll identity through spreading, cutting, bundling, sewing, and packing when shade separation is required. Mixing acceptable rolls without a grouping rule can still create visible panel differences on one cap.
Define the number of rolls checked, the locations measured within each roll, and the rule for creating shade groups. State whether panels for one cap must come from the same roll or approved group. Mark held material clearly and keep it away from released lots.
During the documented cap production process, compare first output with the signed sample before the full line proceeds. Repeat the check after a material lot, thread, transfer film, press setting, or supplier changes.
Control logo, thread, and trim color by process
Embroidery thread, screen ink, heat-transfer film, woven patches, silicone, rubber, and molded trims need separate standards. Thread sheen and stitch direction can create apparent light and dark zones. A dense embroidery fill may also change the way the base panel sits and reflects light.
Approve decoration at the intended artwork size, stitch density, backing, base color, press temperature, dwell time, pressure, and film layer. Keep the vector artwork and named color references with the trial. See the خيارات تخصيص الغطاء for the processes that should be identified during development.
For coordinated colors across different processes, define whether the goal is an instrument match, a visual family, or an intentional contrast. Record that decision so the supplier does not chase an impossible numerical match between unlike surfaces.
Carry the approved range into bulk quality control
Bulk inspection should compare the correct style, color, component, and lot with the current approved standard. Record actual readings rather than pass or fail alone. Photograph visible defects under controlled conditions as supporting evidence, while keeping the physical standard and instrument record as the decision base.
| Stage | Sample reviewed | Release decision | Record |
|---|---|---|---|
| Material development | Lab dips and candidate articles | Select the color route and supplier article | Submission history and approved standard |
| Decoration trial | Thread, transfer, print, patch, or molded part on the intended base | Release process settings and color reference | Signed panel and process sheet |
| Pre-production sample | Complete cap made from released materials | Authorize bulk setup | Signed cap, readings, and revision |
| Incoming bulk | Defined rolls and component lots | Release, group, hold, or replace | Lot map and measurement file |
| Line and final inspection | Assembled caps across defined lots | Continue, correct, rework, or hold | Inspection report and disposition |
Color records belong in the broader sample-to-bulk quality control plan. If a lot fails, confirm the standard revision, specimen identity, conditioning, setup, calibration status, and calculation before deciding on re-dyeing, replacement, re-cutting, or a documented concession.
Make the purchase decision before order release
Confirm the physical standard, component map, measurement formula, setup, visual light source, tolerance rule, shade grouping, sample stages, bulk frequency, and release authority. Check that the approved shell, visor, mesh, sweatband, thread, logo, piping, closure, and labels match the planned bill of materials.
Ask who owns each standard, where it is stored, how revisions are controlled, and what happens after a failed result. The purchase order should point to the current specification and signed sample. A change in material supplier, finish, dye route, logo process, or trim source needs the agreed comparison before approval.
A color system works when development, sourcing, the laboratory, the factory, and final inspection use the same references and decision rules. That discipline reduces subjective arguments and helps keep repeated orders visually consistent.
Frequently asked questions
Is color tolerance the same as colorfastness?
No. Color tolerance judges the match between a specimen and an approved standard at inspection. Colorfastness measures change or staining after a defined exposure. Use separate requirements and reports.
Can a brand approve color from a phone photograph?
A photograph can support communication, though it is unreliable as the sole production standard. Camera processing, screen settings, compression, and room light alter appearance. Use a controlled physical standard and recorded measurement setup.
Should every cap component use the same numerical limit?
Only when the brand has confirmed that the comparison and limit suit those materials and surfaces. Woven fabric, mesh, thread, silicone, plastic, and reflective transfers may need separate standards and acceptance rules.
What should a color report name?
Name the standard, specimen, material lot, instrument, geometry, aperture, illuminant, observer, backing, orientation, measurement count, formula, parameter settings, individual readings, summary, limit, and decision.
How should bulk rolls be handled after approval?
Keep roll and lot identity, inspect at defined positions, create shade groups under the approved rule, and prevent unapproved mixing during cutting and sewing. Retain readings and the release decision with the order record.
What should a buyer send for a color-tolerance review?
Send the brand color references, style drawing, component map, material and finish details, target markets, logo artwork, decoration processes, prior standards, proposed measurement method, sample stages, order quantities, destination, and required delivery date.
If you are preparing an RFQ, contact JoinTop with your brand or website, cap style, quantity per style and color, vector logo file, target market, destination, required delivery date, material plan, and color references. Use the inquiry form at the bottom so the team can review lab dips, decorated samples, approval records, and bulk shade controls.

 AR
 EN
 ES
 FR
 JA
 KO
 RU
 DE
 PT
 IT
 TR